


Views: 261 Author: CNDY-Press Publish Time: 2026-08-12 Origin: Site


Content Menu
● What Is Offline Press Brake Programming?
● What Is On-Machine Programming?
● Offline Programming vs. On-Machine Programming
● The Real Cost of Idle Press Brake Time
● When Offline Programming Creates the Greatest Value
>> Repeat Orders and Product Families
>> Large Panels and Difficult Handling
● When On-Machine Programming Is the Better Choice
>> Simple Parts
● Build a Hybrid Programming Workflow
>> Step 1: Classify Production Jobs
>> Step 2: Program Complex Work Offline
>> Step 3: Prepare Tooling Before Setup
>> Step 4: Transfer the Program to the Machine
>> Step 5: Run First-Part Inspection
>> Step 6: Capture Operator Knowledge
● The Most Overlooked Requirement: Accurate Tooling Data
● FAQ
>> 1. Can offline programming completely replace press brake operators?
>> 2. Is offline programming useful for small workshops?
>> 3. Does offline programming reduce scrap?
>> 4. What information is required to create an offline bending program?
>> 5. What is the biggest challenge when implementing offline programming?
A CNC press brake is often one of the most important assets in a sheet metal workshop. It affects delivery schedules, labor utilization, part quality, and overall production capacity.
When the machine is bending finished parts, it generates value. When it is idle during program creation, tool selection, collision troubleshooting, or trial bending, capacity is lost.
This makes the programming method an important production decision.
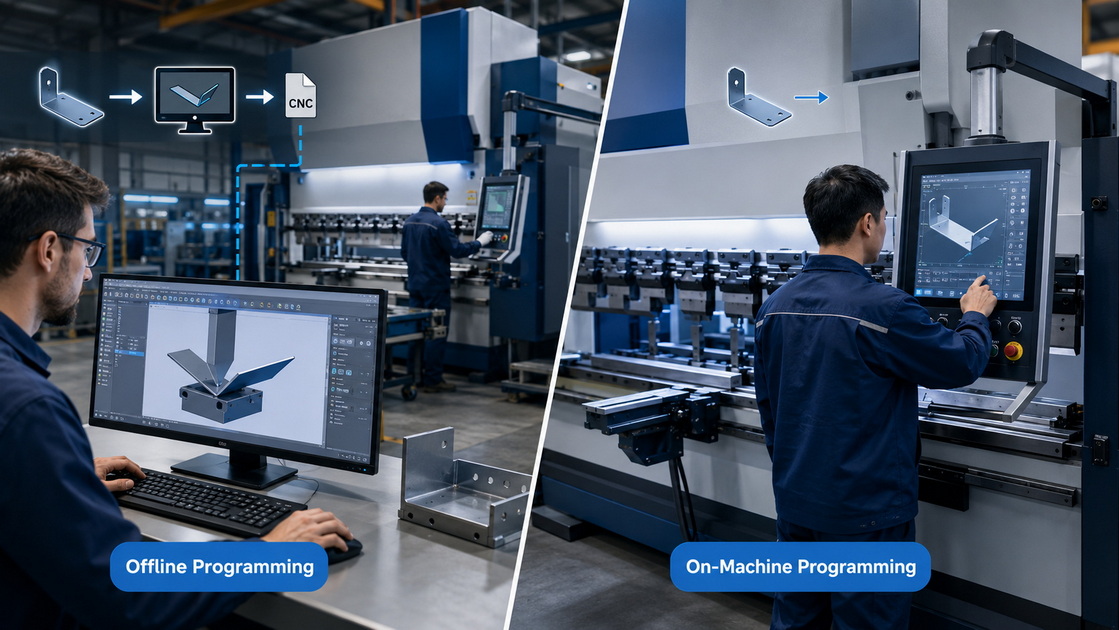
Offline programming allows engineers or programmers to prepare bending programs away from the press brake. They can import drawings, select tooling, calculate bend sequences, simulate part movement, and create setup instructions before the job reaches the production floor.
On-machine programming takes place directly at the press brake controller. The operator enters dimensions, bend angles, tooling data, and backgauge positions, then creates and adjusts the program while standing at the machine.
Neither method is universally better. The right approach depends on part complexity, order quantity, material variation, operator experience, tooling availability, and customer delivery requirements.
For manufacturers using CNC press brakes in high-mix production, the most effective approach is usually a structured combination of both methods.
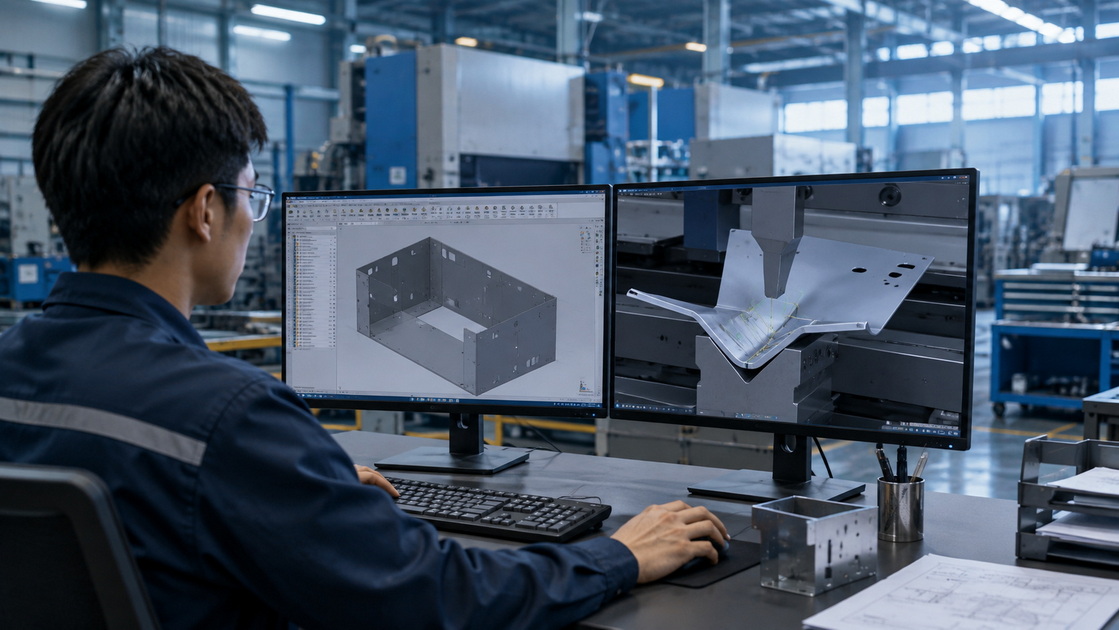
Offline press brake programming is the process of creating bending programs with dedicated software on a computer workstation rather than at the machine controller.
The workflow usually begins with a 2D drawing, DXF file, STEP file, or 3D CAD model. The programmer uses the software to define the material, thickness, bend angles, tooling, bend sequence, and machine configuration.
A complete offline program may include:
- Part geometry and dimensions
- Material type and thickness
- Bend allowance and bend deduction data
- Punch and die selection
- Tool station arrangement
- Backgauge positions
- Bend sequence
- Part rotation direction
- Collision checks
- Operator setup sheets
- CNC program output
The main benefit is simple: the press brake can continue producing parts while programming work happens elsewhere.
For factories with frequent order changes, this can improve production flow significantly. Instead of waiting at the machine for an operator to interpret a drawing and test possible bend sequences, the operator can receive a prepared job package.
That package may include the program file, tooling layout, bend sequence, part orientation, material notes, and inspection requirements.
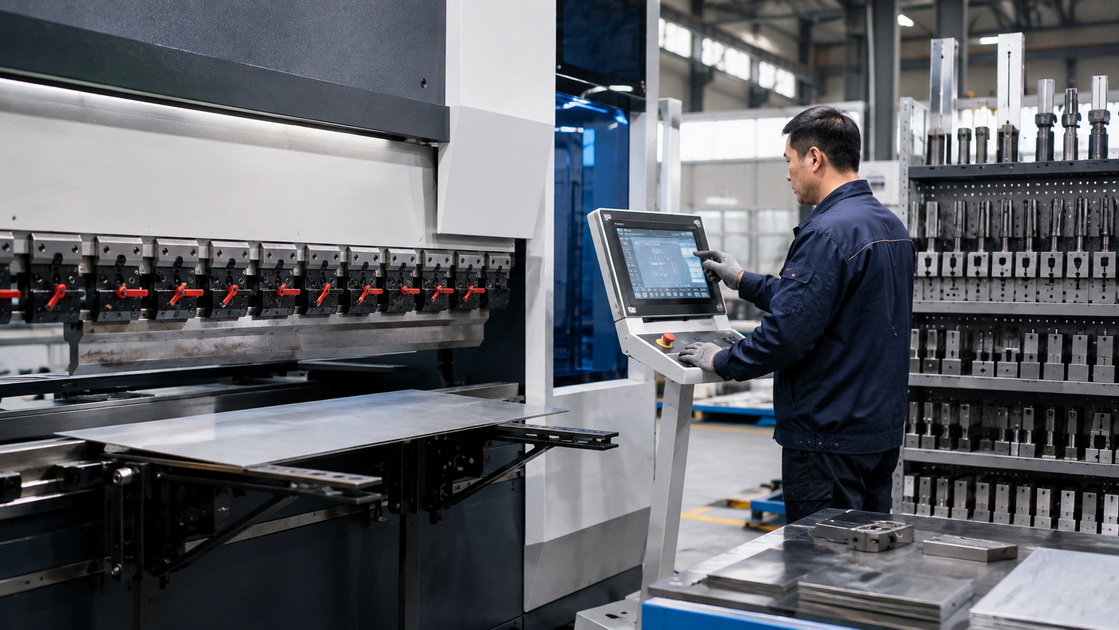
On-machine programming is the traditional method of creating a press brake program directly through the CNC controller.
The operator inputs the required dimensions and bend angles, chooses tooling parameters, sets the backgauge, performs trial bends, and adjusts the program based on actual material behavior.
Modern CNC controllers can simplify this process through graphical programming screens, 2D visualization, angle correction functions, stored tooling libraries, and program memory.
On-machine programming is commonly used for:
- Simple angle brackets
- Basic U-channels
- Short production runs
- Emergency replacement parts
- Repair work
- Urgent customer modifications
- First-time sample parts
- Small manual adjustments to proven programs
For basic parts, programming at the machine can be fast and practical. An experienced operator may create a simple program in only a few minutes.
However, the situation changes when parts have multiple bends, narrow flanges, complicated geometry, expensive materials, or strict dimensional requirements. In those cases, the operator may need several trial attempts before reaching a stable production setup.
During that time, the machine is unavailable for other work.
| Factor | Offline Programming | On-Machine Programming |
|---|---|---|
| Programming location | Engineering workstation | CNC press brake controller |
| Machine availability | Higher during planning | Reduced during program creation |
| Suitable part complexity | Medium to high | Low to medium |
| Collision detection | Advanced simulation possible | Depends on controller and operator experience |
| Tooling preparation | Completed before machine setup | Often completed during setup |
| Operator dependence | Lower for program creation | Higher for complex parts |
| First-part readiness | Strong when data is accurate | Depends on trial bends and experience |
| Best production environment | High-mix, repeat, complex, automated work | Simple, urgent, low-volume work |
| Investment requirement | Software, training, data preparation | Usually available with existing controller |
| Shop-floor flexibility | Strong for planned jobs | Strong for immediate changes |
Many manufacturers focus mainly on bending speed. They compare strokes per minute, tonnage, backgauge speed, and machine price.
These factors matter, but production loss often happens before the first production part is bent.
Common non-productive activities include:
- Creating a bending program at the controller
- Looking for tools
- Checking punch and die compatibility
- Testing bend direction
- Reworking incorrect flange lengths
- Adjusting angle compensation
- Resolving part collisions
- Waiting for drawing clarification
- Repeating setup procedures
- Rebuilding programs for repeat orders
A press brake may appear active throughout the shift, but much of that time may not create finished parts.
A useful internal metric is:
Press Brake Uptime=Productive Bending Time/Available Machine Time×100
For example, if a press brake is available for 480 minutes during a shift but spends 75 minutes on program creation, setup corrections, and trial bending, the machine has only 405 minutes available for productive bending.
Offline programming does not remove every setup task. Operators still need to load material, install tooling, confirm safety conditions, and inspect the first part.
However, it can move planning, simulation, and documentation work away from the press brake.
Complex parts are where offline programming can make the biggest difference.
A sheet metal component with six, eight, or twelve bends may require careful planning. The part may interfere with the press brake frame, punch, die, backgauge fingers, clamps, or safety system during a poorly planned bend sequence.
Potential problems include:
- Collision between formed flanges and tooling
- Collision with the upper beam
- Backgauge interference
- Incorrect part rotation
- Unstable material support
- Difficult manual handling
- Tool segmentation conflicts
- Surface scratches
- Wrong bend sequence
- Insufficient clearance for the operator
Offline simulation allows the programmer to test different bend sequences before production begins. This reduces the risk of discovering major problems after the machine has already been set up.
High-mix production creates frequent changeovers. A shop may process dozens of different part numbers in one shift, each with different materials, thicknesses, tools, bend requirements, and inspection standards.
In this environment, setup preparation becomes a major productivity advantage.
Offline programming allows the engineering team to prepare jobs before they reach the production floor. The operator receives a structured package rather than a drawing that must be interpreted from the beginning.
A prepared production package can include:
- Finished CNC program
- Tooling list
- Tool station layout
- Bend sequence
- Material information
- Part orientation guide
- First-part inspection requirements
- Notes for special handling
This approach reduces variation between operators and makes repeat production more reliable.
Repeat jobs are ideal candidates for offline programming.
Once a part has been validated, the factory can store the approved program, tooling configuration, setup instruction, and actual correction values in a digital library.
The next production run becomes faster because the operator does not need to rebuild the process from memory.
This is especially valuable for:
- Electrical cabinets
- HVAC components
- Elevator panels
- Stainless steel enclosures
- Agricultural equipment covers
- Machinery guards
- Construction equipment panels
- Storage systems
- Industrial control boxes
- Metal furniture components
A well-maintained program library can become one of the most valuable production assets in a fabrication shop.
Large panels create additional challenges because the operator must consider part weight, rotation space, flange interference, and material stability.
Offline simulation can help identify whether a part requires:
- Additional front supports
- A second operator
- Material handling equipment
- Special bending order
- Segmented tooling
- Modified backgauge settings
- Alternative tooling
- A different press brake configuration
This improves both efficiency and shop-floor safety.
For robotic or automated bending systems, offline programming is often essential.
An automated cell must coordinate more than a press brake program. It must manage part loading, gripping, rotation, tool clearance, robot movement, stack position, unloading, and collision prevention.
The programming process must account for:
- Robot gripper position
- Part pickup direction
- Material orientation
- Tooling layout
- Part center of gravity
- Robot travel path
- Machine opening height
- Bend sequence
- Unloading clearance
- Finished-part stacking
Offline planning helps manufacturers identify automation problems before production starts.
For a basic part with one or two bends, direct programming at the CNC controller can be faster than preparing a separate offline file.
A skilled operator can often complete the program quickly for:
- L-brackets
- U-channels
- Small mounting plates
- Simple covers
- Repair components
- Sample pieces
- Short flanges
- Low-risk mild steel parts
In these cases, using offline software may create unnecessary administration.
Production schedules are rarely perfect. Customers may revise drawings, material may change, or an urgent replacement part may be needed immediately.
On-machine programming provides flexibility when fast decisions are required. The operator can make controlled changes directly at the press brake without waiting for a separate programming process.
Material behavior can vary even when the nominal thickness is the same.
Bend results can be affected by:
- Tensile strength variation
- Material grain direction
- Surface coating
- Film protection
- Material hardness
- Thickness tolerance
- Punch radius
- Die opening
- Tool wear
- Temperature conditions
Offline software provides a strong starting point, but real material behavior must still be confirmed through first-part inspection.
This is why skilled operators remain essential. They translate digital preparation into accurate physical production.
The strongest approach is not to choose one method for every job. It is to use a controlled hybrid workflow.
Separate incoming work into categories:
- Simple parts
- Complex parts
- Repeat orders
- Urgent jobs
- High-value materials
- Large panels
- New-product introduction
- Automated-cell projects
This prevents the factory from using the same programming method for every job.
Use offline programming for jobs with high collision risk, multiple bends, expensive material, complex tooling, or repeat production potential.
The goal is to complete as much planning work as possible before the press brake becomes involved.
Tooling should be ready before the job reaches the machine.
The operator should receive a clear list of:
- Punches
- Dies
- Tool lengths
- Tool positions
- Required clamps
- Setup order
- Material thickness
- Safety notes
This reduces time spent searching for tools and rebuilding setups.
Before production starts, confirm that the program matches the actual press brake configuration.
Check:
- Controller compatibility
- Machine tonnage
- Bed length
- Tooling arrangement
- Backgauge configuration
- Crowning system
- Clamp type
- Safety devices
- Material specification
A program should never be treated as automatically correct simply because it was generated by software.
The first part should be inspected before full production begins.
Key checks include:
- Bend angle
- Flange length
- Overall dimensions
- Diagonal measurements
- Hole-to-bend position
- Flatness
- Surface quality
- Scratch marks
- Part orientation
- Assembly fit
The results should be recorded and used to update the master program when necessary.
Operators often identify practical production improvements that engineering teams cannot see from a computer workstation.
For example, an operator may discover:
- A more stable part rotation method
- A safer handling sequence
- A better tool arrangement
- A more consistent angle correction
- A faster setup order
- A material-specific adjustment
These improvements should be documented. The best production libraries combine engineering data with real shop-floor experience.
Offline programming is only as reliable as the data entered into the system.
A common mistake is to use generic or incomplete tooling libraries. If the software model does not match the actual press brake, punch, die, clamps, backgauge fingers, or safety devices, the simulation may look correct while the physical setup fails.
Before implementing an offline workflow, verify:
- Press brake tonnage
- Working length
- Daylight opening
- Stroke length
- Throat depth
- Backgauge travel
- Finger geometry
- Crowning system
- Punch profile
- Die profile
- Tool height
- Tool segmentation
- Clamping system
- Front support configuration
- Safety guarding
- Material database
For customized CNC press brake projects, this information should be considered during equipment selection and technical confirmation.
A machine designed for connected production should support consistent tooling, clear controller communication, organized program transfer, and reliable operator setup.
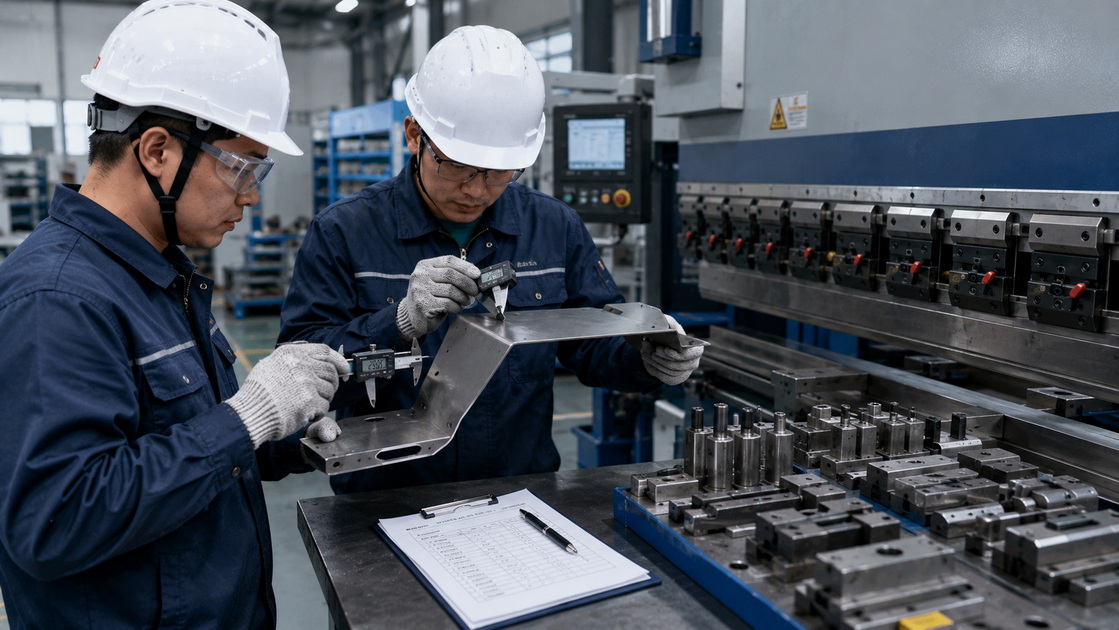
Offline programming is most valuable when part complexity, repeatability, setup reduction, collision prevention, and production scheduling are important.
On-machine programming remains valuable for simple parts, urgent corrections, short runs, and real-world adjustment after the first bend.
The most productive fabrication shops do not force every job into one process. They prepare complex work offline, validate it on the press brake, record the proven adjustments, and use those lessons to improve future jobs.
CNDY-Press supports press brake buyers, sheet metal equipment distributors, and OEM partners with customized CNC press brake solutions, integrated fabrication equipment, and configuration support based on actual production requirements. Share your material type, thickness range, bending length, part complexity, tooling preference, and output target to develop a more suitable equipment plan.
No. Offline programming reduces programming and setup work at the machine, but experienced operators are still needed for tooling installation, first-part verification, material handling, safety checks, and practical angle correction.
Yes, especially for workshops producing repeat parts, complicated enclosures, high-value materials, or frequent product changes. For shops that only bend simple brackets, direct controller programming may remain sufficient.
It can reduce scrap by identifying possible collisions, incorrect bend sequences, tooling conflicts, and handling issues before the first physical part is made. Material variation still requires first-part inspection.
The programmer needs part drawings or models, material type, thickness, bend requirements, machine model, controller information, tooling data, backgauge details, crowning configuration, and safety limitations.
The biggest challenge is often inaccurate machine and tooling data. A digital model must match the actual punch, die, clamps, backgauge, press brake geometry, and safety system.
1. [CNDY-Press Company Profile and Sheet Metal Equipment Solutions] [cndypress]
2. [OSHA Power Press Brake Operations and Safeguarding Requirements] [osha]
3. [OSHA Safeguarding by Distance for Power Press Brake Operations] [osha]
4. [The Fabricator Press Brake Safeguarding Overview] [thefabricator]
5. [E-CI Offline Press Brake Programming Overview] [e-ci]
6. [E-CI CI Bend Programming and Simulation Software] [e-ci]
7. [Durmazlar Offline 3D Press Brake Simulation Features] [durmazlar.com]
8. [SigmaNEST SigmaBEND AP Press Brake Programming Software] [sigmanest]
9. [Metamation Offline Press Brake Programming Guide] [metamation]


