


Views: 201 Author: CNDY-Press Publish Time: 2026-08-09 Origin: Site


Content Menu
● Deep Box Bending and Shallow Bending Compared
● Understanding Deep Box Bending Geometry
>> Why Final Bends Are More Difficult
>> Ram Stroke and Working Clearance
● Tooling Requirements for Deep Box Bending
>> Tall Punches and Punch Extenders
>> Gooseneck Punches for Return Flanges
>> Acute Tooling and Overbend Clearance
● Shallow Bending Requirements and Advantages
>> Why Shallow Bending Is Usually Simpler
>> Variables That Still Matter
● Machine Stroke, Open Height, and Throat Depth
● A Practical Deep Box Bending Workflow
>> 1. Prepare Complete Part Information
>> 2. Review the Bend Sequence
>> 3. Calculate the Full Tool Stack
>> 4. Approve a Physical Sample
● An Overlooked Risk: Ram Clamp Interference
● Selecting a CNC Press Brake for Deep Box Work
>> 1. What is deep box bending?
>> 2. Why is ram stroke important for deep box bending?
>> 3. Do all deep boxes require a gooseneck punch?
>> 4. Can a standard press brake bend deep boxes?
>> 5. How is required press brake opening calculated for a deep box?
Deep box bending and shallow bending may both use a CNC press brake, but they differ significantly in tooling requirements, machine stroke, open height, and production complexity.
A shallow tray or bracket can often be formed using standard punches and V-dies on a conventional press brake. A deep box, however, may require tall punches, gooseneck tooling, additional machine opening, longer ram stroke, careful bend sequencing, and a detailed collision-clearance review.
For press brake buyers, the deepest part may be more important than the thickest part. A machine can have sufficient tonnage for the material but still be unable to complete the final bends because formed walls collide with the punch, ram clamp, die, backgauge, or machine frame.
CNDY-Press manufactures CNC press brakes and integrated sheet-metal processing equipment for fabrication businesses. For OEM and ODM projects, machine configuration should be based on the geometry of the most difficult production parts rather than only tonnage and bending-length requirements.

Shallow bending usually involves low flange heights, open profiles, simple channels, brackets, trays, panels, and single-angle bends. The workpiece can normally rotate freely around the punch and die during the bending sequence.
Deep box bending involves forming multiple high sidewalls around a sheet-metal part. During the third and fourth bends, the previously formed walls may interfere with the press brake tooling or upper beam. The workpiece may need to be held at an angle while final flanges are formed, making clearance a critical concern.
| Factor | Shallow Bending | Deep Box Bending |
|---|---|---|
| Typical part geometry | Brackets, panels, channels, shallow trays | Deep trays, cabinets, enclosures, electrical boxes, housings |
| Flange height | Low to moderate | High relative to the part width |
| Tooling requirements | Standard punches and V-dies are often sufficient | Tall punches, gooseneck punches, extenders, and specialty dies may be required |
| Machine stroke | Standard stroke may be suitable | Longer stroke is often required |
| Open height | Moderate clearance is often acceptable | Large open height is frequently essential |
| Collision risk | Lower | Higher during the third and fourth bends |
| Bend sequencing | Usually straightforward | Requires planned bend order and clearance review |
| Production setup | Faster and simpler | More complex and often more time-consuming |
| Machine-selection priority | Tonnage, bed length, and basic tooling | Open height, stroke, throat depth, tooling height, and clearance |
The key difference is clearance. During deep box bending, the formed walls must move around the punch, die, clamps, and machine structure without interference.
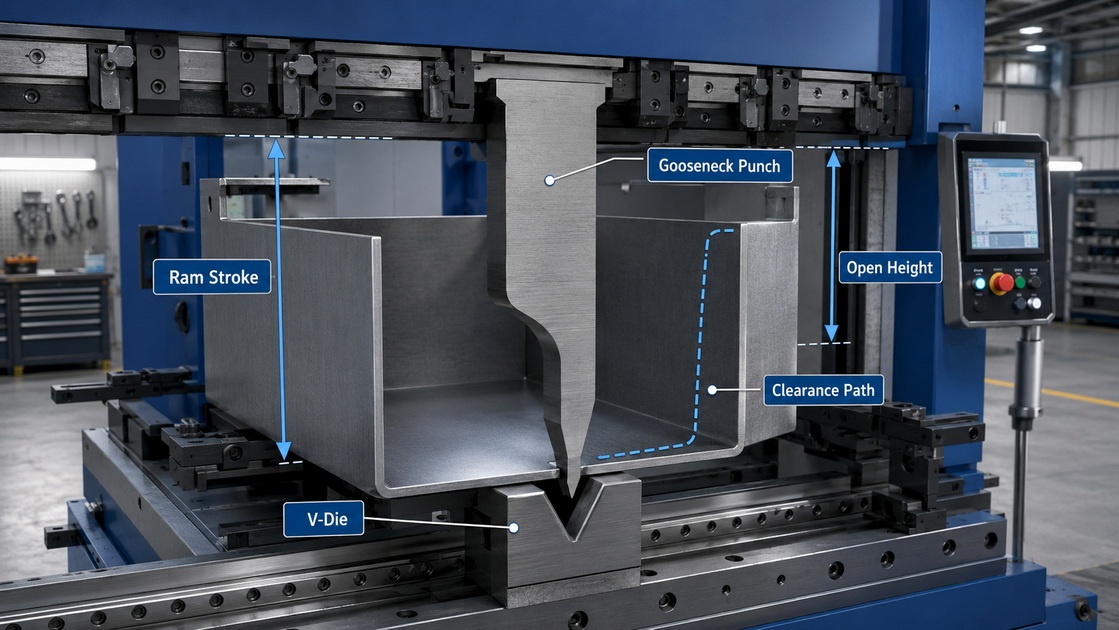
A deep box is generally a four-sided sheet-metal part with relatively tall walls. Common applications include electrical enclosures, industrial cabinets, machine guards, battery housings, HVAC components, equipment covers, fabricated containers, and stainless-steel trays.
The first and second bends are usually manageable. The real challenge appears during the third and fourth bends, when the existing sidewalls must rotate through the available space inside the press brake.
When creating a four-sided box, the final bends often position the part diagonally inside the machine. Previously formed walls can contact the upper punch, ram clamp, lower die, backgauge fingers, or press brake frame.
This can create several practical problems:
- The punch is too short for the box depth
- The machine lacks sufficient open height
- The ram stroke is too limited
- The formed wall hits the punch body
- The workpiece contacts the ram clamp
- The backgauge fingers interfere with the part
- The operator has limited room to guide the workpiece
- The bend sequence creates an unavoidable collision
- The selected tooling does not provide enough overbend clearance
A deep-box project should begin with the part drawing, material details, and full tooling stack. The press brake should then be evaluated against the required clearance during every bending stage.
Machine daylight, often called open height, is the maximum vertical clearance between the ram and the bed when the ram is fully raised.
For deep box bending, the open height must accommodate:
- Lower die height
- Die holder height
- Punch height
- Punch holder or clamping-system height
- Material thickness
- Formed wall depth
- Safe loading and unloading clearance
A press brake may have enough bed length and tonnage but still be unsuitable for a deep box if the available opening is too limited.
Ram stroke is the vertical travel distance of the upper beam. It affects how far the punch can move downward into the die and how far the ram can retract to provide clearance for tooling and finished parts.
A longer stroke can support:
- Deep tooling setups
- Tall punches and extenders
- Large box depths
- Acute-angle tooling
- Easier part loading and removal
- Complex bend sequences
- Better clearance during final bends
However, stroke alone does not solve all deep-box problems. Open height, tool-stack height, throat depth, punch shape, die design, and part rotation space must be reviewed together.

Tooling often determines whether a deep box can be formed efficiently and safely.
Deep box bending often requires taller punches than shallow bending. A tall punch creates more vertical clearance for formed sidewalls to pass beneath or around the upper tooling during later bends.
Punch extenders can increase working height when standard punches are not tall enough. However, every added component consumes part of the machine's available opening.
Before selecting an extender, confirm:
- Total punch and holder height
- Clamping-system height
- Tool alignment requirements
- Tool load capacity
- Machine open height
- Compatibility with the lower die
- Safe setup and changeover method
The full punch assembly must fit the machine while leaving enough space for the deepest formed wall.
A gooseneck punch has a relieved profile that provides clearance for already formed flanges and walls. It is commonly used when a straight punch would collide with the workpiece.
Gooseneck punches can be useful for:
- U-shaped profiles
- Return flanges
- Channels
- Deep boxes
- Electrical enclosures
- Multi-bend sheet-metal parts
The relieved shape can reduce tool strength compared with a straight punch of the same height. The selected tooling should therefore be checked for material thickness, bend length, required tonnage, and operating load.
Acute-angle punches and dies may be used when a deep-box part requires additional clearance or when springback requires overbending.
Acute tooling can be versatile for air-bending applications, but it must be selected based on material thickness, tensile strength, bend radius, required angle, and tooling load capacity.
The tool set should support the full bending sequence rather than only the first bend.
The V-die opening affects bending force, inside bend radius, flange support, and final surface appearance.
A common starting point for air bending mild steel is to use a V-die opening around eight times the material thickness. This is not a universal rule. Material type, desired radius, punch angle, finish requirements, and part geometry may require a different opening.
A die opening that is too small can increase required tonnage and create surface marks or cracking. A die opening that is too large can reduce control over the bend radius and may create issues with short flanges.
Shallow bending includes parts with lower sidewalls, shorter flanges, and more open profiles. Typical examples include mounting brackets, panel edges, shallow trays, channels, tabs, covers, and simple formed components.
These parts usually require less vertical clearance and can be produced with standard punch-and-die combinations.
Shallow bending may offer several production advantages:
- Lower tooling complexity
- Faster setup
- Lower collision risk
- Easier operator handling
- Wider availability of standard tools
- Shorter programming time
- Better compatibility with conventional machine configurations
- Lower tooling cost for small production runs
A standard straight punch and V-die may be sufficient for many shallow parts. This can reduce investment and make production changeovers faster.
Shallow bending still requires proper process control. Important variables include:
- Material thickness and grade
- Material grain direction
- Minimum flange length
- Required bend radius
- Springback
- Tooling condition
- Backgauge position
- Bend sequence
- Surface-protection requirements
Thin stainless steel, aluminum, painted sheet, and decorative materials may require specialized tooling or protective film even when bend depth is limited.
For deep-box applications, three machine dimensions should always be evaluated together: ram stroke, open height, and throat depth.
| Machine Feature | Primary Function | Importance for Deep Box Work |
|---|---|---|
| Ram stroke | Vertical travel of the upper beam | Provides movement for deep tooling and formed-wall clearance |
| Open height | Maximum vertical space between ram and bed | Must accommodate the full tooling stack and formed sidewalls |
| Throat depth | Horizontal distance from ram centerline to frame | Determines whether wide or deep parts clear the machine frame |
| Bed length | Usable bending length | Must match part width and tooling requirements |
| Tonnage | Available bending force | Must support material, bend length, die opening, and bending method |
| Backgauge travel | Rear positioning range | Supports repeatability and complex part setup |
| Crowning system | Compensation for machine deflection | Helps maintain angle consistency across long bends |
A long-bed press brake with limited throat depth may not handle wide box components effectively. A high-tonnage machine with insufficient open height may be unable to complete deep final bends.

A structured engineering process can reduce clearance problems, tooling errors, and sample failures.
Provide the press brake supplier with:
- 2D production drawings
- 3D CAD models
- Material type and grade
- Material thickness
- Box depth and width
- Bend angles
- Inside-radius requirements
- Expected production volume
- Surface-finish requirements
- Existing-tooling information
The deepest and most complex component should guide machine selection.
A four-sided box should not automatically be bent in the same order for every design. The sequence can determine whether the part clears the tooling.
Review:
- Which bends should be completed first
- Whether long sides should be formed before short sides
- Whether the part must be tilted for the final bends
- Whether tool segmentation is necessary
- Whether backgauge fingers could interfere
- Whether the operator has safe loading space
- Whether a gooseneck or special punch profile is required
For complex projects, bending simulation can help identify collisions before material is cut.
The tool stack includes more than the punch and die.
Calculate:
- Punch height
- Punch holder or clamping height
- Extender height, if used
- Die height
- Die holder height
- Material thickness
- Required formed-wall clearance
- Machine open height
This calculation should be completed before ordering tooling or confirming the machine model.
A physical sample is essential for deep box bending. Digital models are valuable, but real material can behave differently because of springback, thickness variation, surface coatings, operator handling, and practical clearance limits.
The sample should be checked for:
- Interference during every bend
- Final dimensions
- Bend-angle repeatability
- Tool marks
- Sidewall squareness
- Safe operator handling
- Loading and unloading time
- Repeat-production feasibility
Many buyers focus on the punch and die but overlook the ram clamping system.
In deep-box applications, the formed wall may clear the punch body but still hit the punch holder, manual clamp, hydraulic clamp, or upper beam. This is a common reason why a design that looks feasible in a simplified drawing fails during an actual bending trial.
Before approving a machine or tool setup, request a complete clearance review that includes:
- Punch profile
- Punch-holder geometry
- Manual, pneumatic, or hydraulic clamp profile
- Ram shape
- Machine open height
- Formed-wall movement during final bends
- Backgauge-finger position
- Operator loading space
The best time to identify clamp interference is before production begins.
A CNC press brake for deep box bending should be configured around the real production geometry.
Important specifications to discuss include:
- Required tonnage and bending length
- Maximum box depth
- Required open height
- Required ram stroke
- Throat depth
- Crowning configuration
- CNC controller and axis requirements
- Backgauge design
- Tooling type and total tooling height
- Clamping system
- Safety configuration
- Front support or sheet-following requirements
- Automation and material-handling needs
CNDY-Press supports customized CNC press-brake configurations and OEM or ODM manufacturing projects. Machine design can be adapted around bed length, tonnage, CNC control, backgauge configuration, tooling, safety requirements, and supporting sheet-metal equipment.
Deep box bending and shallow bending require different levels of machine capability, tooling investment, and production planning.
Shallow bends can often be formed with standard tooling and conventional press-brake configurations. Deep boxes require a more detailed review of punch height, tooling profile, machine stroke, open height, throat depth, and bend sequence.
The most reliable approach is to provide complete part geometry before selecting a press brake. A clearance review, tooling calculation, bend simulation, and physical sample can prevent costly interference problems during production.
For fabrication businesses producing deep enclosures, cabinets, trays, and complex sheet-metal parts, CNDY-Press can support customized CNC press-brake configurations, tooling discussions, and OEM or ODM manufacturing requirements.
Deep box bending is the process of forming sheet-metal boxes or enclosures with sidewalls tall enough to create tooling and machine-clearance challenges during the final bends.
Ram stroke determines how far the upper beam can travel. A longer stroke can provide additional room for tall punches, deep sidewalls, and more complex final-bend operations.
No. A gooseneck punch is useful when formed flanges or walls would collide with a straight punch. The correct tooling depends on box depth, bend sequence, material thickness, bend angle, and available machine clearance.
A standard press brake may form deep boxes if it has sufficient open height, stroke, throat depth, tonnage, and compatible tooling. A drawing review, bend simulation, and physical sample should be completed before production.
The calculation should include die height, die holder height, punch height, punch holder height, material thickness, formed-wall depth, clearance requirements, and available machine opening.
1. [CNDY-Press, CNC Press Brake and Sheet Metal Processing Equipment] [cndypress]
2. [Canadian Metalworking, Deep Box Bending Basics] [canadianmetalworking]
3. [The Fabricator, The Rules of Press Brake Tool Selection] [thefabricator]
4. [Approved Sheet Metal, Deep Forming Considerations] [approvedsheetmetal]
5. [Vicla, Mastering Press Brake Tooling] [vicla]
6. [Xometry, Sheet Metal Bending Guide] [xometry]


